
Slurry pumps are an essential part of mining operations, where they handle abrasive, corrosive, and viscous slurries. These pumps play a critical role in transporting mineral ores and processing fluids in mining applications, ensuring efficient and smooth operations. In this article, we will discuss the types of slurry pumps, their components, how they function in mining, and the key considerations for selecting the right pump for different mining tasks.
Slurry Pumps in Mining
Slurry pumps are specifically designed to handle mixtures of solids and liquids, commonly referred to as “slurry.” In mining, slurries can contain a mix of water, mineral particles, and chemicals that require a robust pumping system capable of withstanding the wear and tear caused by abrasive materials.
Slurry pumps are used in several stages of mining operations, from transporting ore from one process to another to the disposal of tailings. The volume of slurry and mining materials would be difficult to handle without these pumps.
Types of Slurry Pumps
There are two primary types of slurry pumps used in mining applications: centrifugal and positive displacement pumps. Each has distinct advantages depending on the nature of the slurry and the requirements of the mining operation.
Centrifugal Slurry Pumps
Centrifugal pumps are the most commonly used type of slurry pumps. These pumps work by converting rotational energy into kinetic energy to move the slurry. As the impeller rotates, it generates centrifugal force, which pushes the slurry through the pump and into the discharge pipe.
Due to their efficiency and capacity to handle large volumes of slurry, centrifugal pumps find widespread use. However, they are best suited for slurries with lower concentrations of solids and lower viscosities, as more abrasive or viscous materials can cause significant wear on the pump components.
Positive Displacement Slurry Pumps
Positive displacement pumps operate differently from centrifugal pumps. These pumps move slurry by trapping a fixed amount of it in a chamber and then displacing it into the discharge pipe. Positive displacement pumps are ideal for high-viscosity slurries or slurries with a high concentration of solids, as they can handle these materials with greater efficiency and less wear.
While positive displacement pumps are highly effective in handling tough slurries, they are generally more expensive and complex to maintain compared to centrifugal pumps.
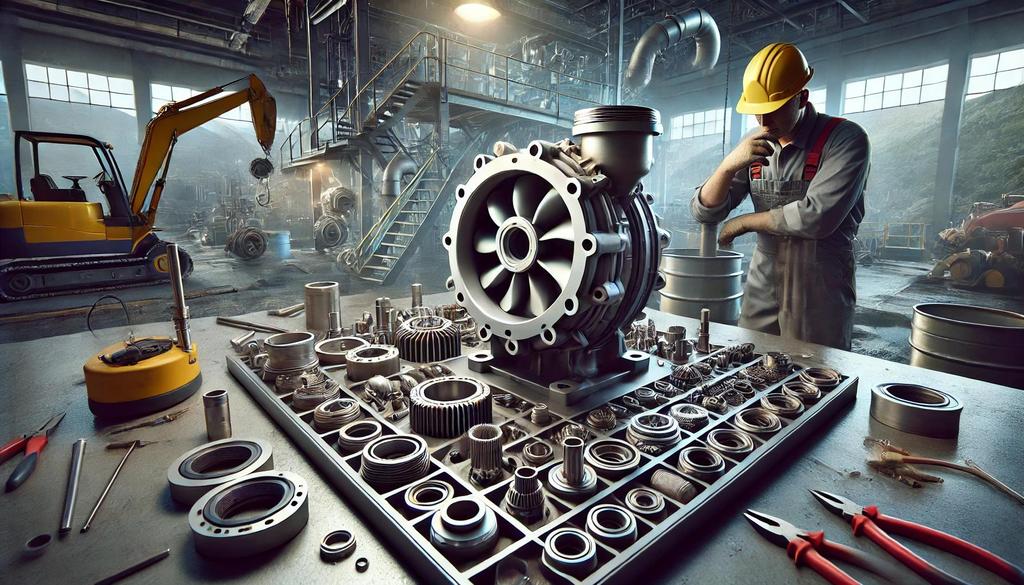
Key Components of Slurry Pumps
Several critical components enable slurry pumps to handle abrasive and corrosive materials. The most important components include:
- Impeller: The rotating part that generates the necessary force to move the slurry.
- Casing: The housing that contains the slurry and directs it through the pump.
- Shaft and Bearings: These components provide support and ensure smooth rotation of the impeller.
- Liners: Protective liners are often added to the casing and impeller to reduce wear and extend the life of the pump.
- Seals: Seals prevent leakage and ensure the pump operates efficiently without losing pressure.
Each of these components is typically made from materials that offer high wear resistance, such as rubber, metal alloys, or ceramics, depending on the specific application.
Applications of Slurry Pumps in Mining
Slurry pumps have a wide range of applications in the mining industry, including:
- Ore Processing: Slurry pumps are used to move ore slurries from one processing stage to another, such as from crushers to grinding mills or from mills to flotation units.
- Tailings Disposal: After the valuable minerals have been extracted, the leftover waste material, known as tailings, is often transported using slurry pumps to storage facilities or for disposal.
- Dewatering: Slurry pumps are also used to remove excess water from mining pits or underground mining areas, ensuring that operations can continue safely and efficiently.
In each of these applications, slurry pumps must be able to handle the specific characteristics of the slurry, such as its abrasiveness, particle size, and viscosity.

Factors to Consider When Choosing a Slurry Pump
Selecting the right slurry pump for a mining application requires careful consideration of several factors. The wrong pump can result in inefficiency, increased wear, and costly downtime.
Pump Material
One of the most important factors to consider is the material of the pump components. For highly abrasive slurries, pumps with wear-resistant materials such as high-chrome alloys or rubber linings are recommended. Corrosive slurries, on the other hand, may require pumps made from stainless steel or other corrosion-resistant materials.
Wear Resistance
Slurries in mining operations often contain sharp, hard particles that can quickly wear down pump components. Selecting a pump with wear-resistant features, such as replaceable liners and impellers, can significantly extend the lifespan of the pump and reduce maintenance costs.
Efficiency and Performance
The efficiency of a slurry pump is critical to the overall performance of a mining operation. Pumps that are too small for the required flow rate or too large for the application can waste energy and reduce operational efficiency. It’s essential to choose a pump that can handle the required flow rate and pressure while minimizing energy consumption.
Maintenance and Troubleshooting of Slurry Pumps
Regular maintenance is crucial to ensure the long-term performance and reliability of slurry pumps in mining. The abrasive nature of slurries means components such as impellers, liners, and seals will wear over time and need to be replaced periodically.
Common maintenance tasks include:
- Checking for wear: Inspecting the impeller, casing, and liners for signs of wear and replacing them as needed.
- Seal maintenance: Regularly checking seals for leaks and ensuring they are functioning properly.
- Bearing lubrication: Ensuring the pump’s bearings are adequately lubricated to prevent overheating and premature failure.
In addition to routine maintenance, it is essential to address common slurry pump issues. Troubleshooting should focus on problems such as:
- Cavitation, which often results from low inlet pressure.
- Other critical concerns include blockages within the pump and excessive vibration.
- Excessive vibration may signal potential misalignment or imbalanced components.
Taking proactive measures to identify and rectify these issues ensures optimal pump performance and longevity.

Future Trends in Slurry Pump Technology
As the mining industry continues to evolve, so too does slurry pump technology. There are several emerging trends that could significantly impact the future of slurry pumping in mining:
- Smart Pumping Systems: Advancements in sensors and control systems are enabling the development of smart slurry pumps that can monitor their own performance in real time. These pumps can detect issues such as wear, leaks, or inefficiencies and alert operators before they lead to downtime or failure.
- Improved Wear Materials: Ongoing research into new materials for pump components is leading to the development of more wear-resistant and corrosion-resistant materials, which could increase the lifespan of pumps in harsh mining environments.
- Energy Efficiency: With the increasing focus on sustainability, there is a growing demand for slurry pumps that can operate with lower energy consumption. Advances in pump design and materials are helping to improve the efficiency of slurry pumps, which reduces the environmental impact of mining operations.
Modern Mining Operation Efficiency Calls for Advanced Slurry Pumps
Slurry pumps are essential components in mining operations. They effectively manage challenging slurries that include abrasive, corrosive, and viscous materials. To maintain optimal performance, it is crucial for mining companies to select the appropriate type of slurry pump. Key considerations should include the pump’s wear resistance and overall efficiency.
Regular maintenance is also vital to preserve pump functionality and to reduce potential downtime. As advancements in technology continue, slurry pumps are evolving. They are becoming more efficient, durable, and intelligent, which enhances their effectiveness in various mining applications. This ongoing improvement significantly strengthens the reliability of slurry transfer processes in the mining industry.
These advancements not only improve operational efficiency but also promote sustainable mining practices. By integrating state-of-the-art slurry pump technology, mining companies can enhance productivity while effectively reducing their environmental impact.


